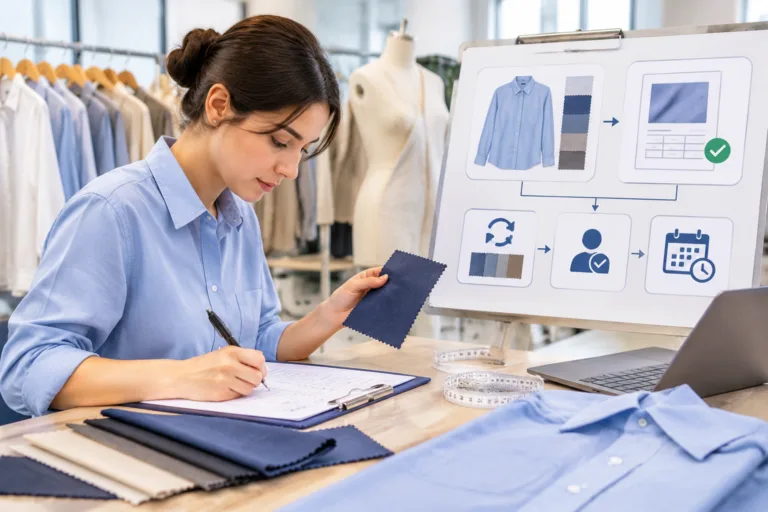
Scaling reactive textile printing from an approved strike-off to bulk production requires more than enlarging the sample. The process depends on locking comparable fabric and artwork inputs, recording the physical color reference, documenting the relevant print and finishing conditions, and comparing bulk output against that reference. This guide is an independent educational resource; the linked Sponsor page does not change its editorial position.
The central idea behind reactive textile printing production controls is controlled replication. A strike-off approves an appearance for a particular artwork, material, color target, and process context. It does not automatically prove that every fabric lot, print run, operator, or finishing condition will produce the same result.
What reactive textile printing production controls must preserve from the approved strike-off
An approved strike-off is a physical reference sample accepted for a defined combination of artwork, fabric, placement, color appearance, and process context. It should be identified with the actual fabric composition, construction, relevant finish, artwork version, print dimensions, placement reference, and color reference. A vague label such as “approved print sample” leaves too much room for comparison against a changed input.
Approval of one sample confirms a visual decision at that point. It is not the same as evidence that bulk production will remain consistent across fabric lots, print runs, operators, or process conditions. Scaling therefore follows a control hierarchy: lock the inputs, monitor the process, then inspect and document the output against the agreed reference.
Material identity is the first control. Fiber content, yarn or fabric structure, fabric color, weight, width, and finish can all affect how a print appears or behaves. Artwork identity is equally important. The record should distinguish file revisions, separations, actual print size, placement coordinates, repeat alignment, and references such as seams, hems, or panel boundaries.
Color approval should rely on the agreed physical reference, not only a screen or monitor. Digital displays vary, and a screen image is not itself a physical color approval. The reference should be available during production inspection, with its condition and identification recorded so that later comparisons do not depend on memory.
Process records should connect the approved sample to the production context. Record the relevant print system, colorant or recipe identity, screens or digital files where applicable, sequence, drying or fixation assumptions, and finishing assumptions. Exact equipment settings, tolerances, wash results, and chemical conditions are project-dependent. They require an agreed method or validated technical source rather than an invented universal specification.
Visual approval also has limits. A close appearance does not by itself establish wash, rub, stretch, heat, or other use-related performance. Those checks need a relevant method and project-specific acceptance criteria. The strike-off is best treated as a controlled reference for decisions, not as a guarantee that variation cannot occur.
Lock the preproduction specification before bulk printing begins
Before bulk printing, align the physical strike-off with a written specification. The artwork record should identify the approved file version, separations, actual print dimensions, minimum detail, color references, repeat or panel alignment, placement coordinates, and revision history. This turns the sample into a reference that another person can interpret rather than an isolated object.
The fabric record needs the same precision. Separate fiber composition from yarn details, fabric construction, weight, width, color, finish, and lot identity. A commercial name such as satin or knit is not a complete material specification. Those terms describe only part of the fabric identity, and materials with the same label can behave differently.
Placement should use practical garment references, including seams, hems, grain or wale direction, and panel boundaries. The purpose is to make the location reproducible and observable. Do not insert a universal placement tolerance unless the project has agreed one. Process documentation should also identify the approved print system, colorant or recipe reference, relevant screens or digital files, sequence, drying or fixation conditions, and finishing assumptions without treating one supplier’s setup as universal.
| Observable input | Why it affects replication | Initial control or decision | Variable that could change the decision |
|---|---|---|---|
| Artwork file, separations, size, and placement | Changes can alter detail, registration, scale, or panel alignment. | Lock the approved revision and record physical reference points. A changed file or placement requires review. | Garment pattern, repeat layout, minimum detail, or production method. |
| Fiber, construction, weight, color, finish, and fabric lot | Material structure and surface can change color appearance, coverage, hand, and dimensional behavior. | Compare bulk fabric with the strike-off material. A materially different input requires compatibility review. | Supplier, lot, finish, fabric preparation, or intended garment use. |
| Print system, recipe identity, sequence, and process record | Different chemistry or process conditions can change the resulting surface and color behavior. | Record the approved process context and review any changed condition before production. | Equipment, operator setup, colorant system, drying, fixation, or finishing. |
| Administrative revision or document correction | A clerical change may not alter the physical production reference. | Correct the record and preserve the revision trail without replacing the approved sample. | Whether the change affects artwork, material, placement, or process content. |
This table is a practical decision aid, not a certification checklist or legal requirement. The key distinction is whether the change affects the physical relationship between the approved sample and bulk production. A corrected document date may need record control only; a changed fabric finish or artwork separation may require renewed review or reapproval.
Control fabric, color, and process variables that can change the bulk result
Reactive printing chemistry interacts with the fiber, fabric structure, and finishing system. Depending on the actual materials and process, a change may contribute to altered shade, migration, inadequate fixation, surface changes, or a different hand. These are compatibility questions, not universal outcomes. The same named printing process cannot be generalized across every fiber, dye, finish, or supplier.
Color matching is also different from matching the complete print appearance. Two samples may look close in shade while differing in coverage, penetration, surface feel, edge sharpness, or behavior after finishing. The inspection record should therefore describe more than color alone. Note visible coverage, detail definition, surface character, and any change after the agreed finishing stage.
Registration and placement depend on more than the artwork file. Separations, fabric movement, stretch or relaxation, machine setup, and garment-panel references can all affect where the image lands and how its parts align. A placement reference tied to a seam or panel boundary is more useful than an isolated measurement whose starting point is unclear.
Consider a lightweight or elastic fabric that receives a finish different from the one used for the strike-off. The appropriate decision is not to assume the sample remains representative. Recheck material compatibility, dimensional behavior, hand, coverage, and placement on the actual finished material. The finish may alter the surface or fabric response, but the exact effect must be established for that material and process combination.
Record the fabric lot and the process conditions used for the first bulk checks. This gives later investigation a defined starting point and helps distinguish an input change from an artwork or setup change. It does not eliminate all variation. It makes the variation easier to compare, discuss, and contain.
Practical reactive printing fabric compatibility checks should remain tied to the real specification. Confirm the fiber, construction, preparation, finish, and color conditions rather than relying on a commercial label. If a recipe, fixation condition, or equipment setting is important to the result, record it from the applicable process documentation. Without validated technical support, describe it as a variable to check, not as a guaranteed setting or performance limit.
Monitor the first bulk output and compare it with the approved reference
First-bulk inspection should compare the production output with the approved physical strike-off, not with memory or a screen image. Check the artwork version, print dimensions, placement references, color appearance, coverage, edge definition, registration, hand, visible defects, and fabric identity. Keep the approved reference accessible under suitable viewing conditions so the comparison remains tied to the agreed sample.
Begin with the first available output that represents the intended bulk process. Record what was inspected and the production context, but do not treat one accepted piece as proof that the entire run will remain stable. Fabric lots, handling, process conditions, finishing, and other inputs can change later output. A project may therefore use continued checks, but the timing and frequency should be defined in the applicable quality procedure rather than presented as a universal requirement.
Separate appearance approval from use-related verification. A print can look close to the strike-off while still requiring separate evaluation for laundering, rubbing, stretching, heat exposure, or another use condition. Select the relevant method and acceptance criteria before ordering when durability matters. Without that defined method, visual inspection cannot establish performance after use.
| Observable input | Implication | Initial decision | Variable that could change it |
|---|---|---|---|
| Artwork version, size, or placement | The output may not represent the approved design or location. | Pause comparison and verify the file, dimensions, and garment reference. | Panel shape, seams, alignment method, or an approved revision. |
| Shade, coverage, or edge definition | Appearance differs even if the motif is recognizable. | Compare with the physical reference and document the deviation. | Fabric color, surface, process condition, or agreed viewing method. |
| Fabric identity or finish | The sample may no longer represent the bulk substrate. | Confirm the lot, construction, finish, and material record before release. | Substitution, preparation, finishing, or lot variation. |
| Hand and surface | Color similarity does not establish comparable surface feel. | Record the difference and check whether the specification addresses it. | Coverage, penetration, chemistry, drying, fixation, or finishing. |
| Durability verification | Visual approval leaves later-use performance unresolved. | Select the applicable test method and project criterion. | End use, care conditions, stretch, heat, and required evidence. |
The inspection record should identify the production date or lot, material identity, process or recipe reference, relevant equipment or line context, observations, images or physical references, and the disposition of any deviation. If artwork, fabric, recipe, finish, or process conditions changed, escalate for review or renewed approval. A confirmed visual difference should not be silently normalized.

Respond to variation without losing the approved production reference
When bulk output differs, begin with a controlled comparison against the approved strike-off. Describe the difference before suggesting a cause: shade, coverage, registration, placement, surface feel, dimensional behavior, or later-use performance. A single symptom rarely proves one cause. The useful question is which input or process context changed, and whether that change affects the approved decision.
Trace the record through the artwork revision, fabric lot and finish, colorant or recipe identity, process sequence, drying or fixation condition, equipment setup, and handling. Compare the affected material with an unaffected reference when one is available. This does not establish causation by itself, but it narrows the variables that require technical review. Keep diagnostic possibilities conditional because substrate, chemistry, construction, and finishing can produce similar visible symptoms.
Containment and root-cause analysis are separate actions. Identify and hold affected material or panels according to the project’s quality process while the comparison is underway. Do not assume that reprinting, adjustment, release, or rejection is universally correct. The appropriate disposition depends on the written specification, the confirmed deviation, the affected quantity, and the applicable quality procedure.
A correction can also change the relationship with the original strike-off. If an adjusted output is accepted, document that decision clearly rather than quietly replacing the original reference. Record the reason, the changed input, the approving decision, and the material or production scope to which it applies. This preserves traceability when a later run is compared with either the original or revised reference.
For example, a print may appear acceptable before finishing and look different afterward. That observation does not identify one definite cause. It does show why the comparison should include the finished material and why process and finishing records matter. Review the fabric lot, surface condition, recipe identity, sequence, and relevant finishing context before deciding whether the issue concerns appearance, hand, dimensional behavior, or later-use performance.
A useful deviation record distinguishes observed fact from interpretation. “Coverage appears lower than the approved reference after finishing” is more actionable than assigning a cause without evidence. Add the inspection context, retain the reference used, and state what must be checked next. This approach supports reactive textile printing troubleshooting while avoiding the promise of perfect uniformity or a universal defect-to-cause map.

Build a repeatable learning loop for future reactive print runs
Before approving a future repeat, review the approved strike-off beside the written bulk specification, material identity, artwork version, process record, inspection observations, and any validated test results. Identify which variables changed and which decisions remain unresolved. A strike-off is a controlled reference, not a universal guarantee. The practical next step is to define the applicable visual checks and, when durability, color, or regulatory claims matter, confirm the relevant technical method and project-specific acceptance criteria before the next run.
Frequently Asked Questions
What does an approved strike-off prove in reactive textile printing?
It proves that a specific artwork, material, color target, placement, and process context were approved for that physical reference. It does not by itself prove that every bulk lot, print run, finish, or later-use condition will match.
Which fabric details should be matched between a strike-off and bulk production?
Match the relevant fiber composition, yarn or fabric construction, weight, width, color, finish, and lot identity. A commercial label such as “knit” or “satin” is not a complete material specification and cannot predict print behavior alone.
Why can bulk reactive printing look different after finishing or washing?
Finishing or washing can change the observed surface, hand, color appearance, coverage, or dimensional behavior. The exact result depends on the material and process combination, so the finished output should be checked under the project’s defined conditions.
When should a change in fabric, artwork, or recipe trigger a new strike-off or reapproval?
Trigger review when the change could affect the approved appearance, placement, compatibility, hand, dimensional behavior, or required performance. The project specification or quality procedure should determine whether comparison, adjustment, a new strike-off, or formal reapproval is appropriate.
What should a bulk-print inspection record include?
Include the production date or lot, material identity, artwork and process references, relevant equipment or line context, inspection observations, images or physical references, and the disposition of deviations. Record changed inputs and approval decisions rather than relying on informal comments.
Can visual approval alone confirm reactive print durability?
No. Visual approval addresses appearance against the reference. Wash, rub, stretch, heat, or other durability performance requires a relevant method, defined conditions, and project-specific acceptance criteria. Without those elements, visual inspection cannot establish later-use performance.