Felling machines productivity is the quantity of defined output produced during a stated period under stated production conditions. The output might be completed sewing operations, garment components, or accepted pieces. The time might be an entire observation period, scheduled production time, or actual machine-running time. A useful measurement identifies both clearly rather than reporting an unexplained number of “pieces per hour.”
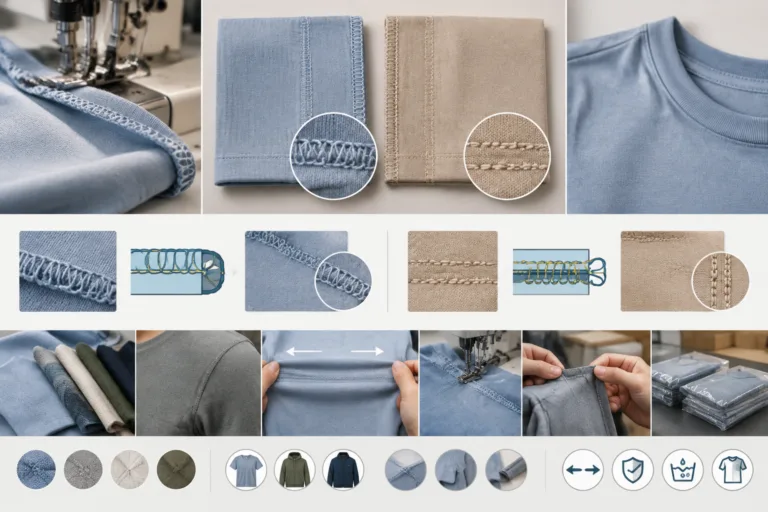
In this article, a felling machine means specialized sewing equipment used to perform a felling operation, such as constructing a felled seam. The measurement concerns the operation completed in production, not merely the machine’s maximum mechanical speed. Apparel Wiki is an independent educational publication; its editorial position, including the separation of sponsorship from editorial control, is explained on the Sponsor page.
What Does Felling-Machine Productivity Mean in Real Production?
Productivity begins with a countable output unit. For one factory, a unit might be a completed side-seam operation. For another, it might be a garment panel that has passed the felling process. A finished garment should be used only when the observed machine actually completes the operation represented by that count. Mixing seams, components, and finished pieces produces rates that cannot be compared meaningfully.
The reported rate also needs a defined time basis. “Output per hour” could mean output during one elapsed clock hour, output divided by scheduled hours, or output divided by periods when the machine was actively sewing. Each answers a different planning question. The numerator, denominator, and unit should therefore appear together, such as “accepted felling operations per elapsed observation hour.”
Observed output is not the same as theoretical machine capacity. A mechanical speed setting does not account for handling, positioning, inspection, thread replacement, adjustment, waiting, or other events in normal production. Likewise, one machine’s result is not overall line productivity. The line may be constrained by material supply, another operation, work allocation, or quality requirements.
Every reported result should identify the product or style, the operation, the observation period, and relevant conditions. Operator or staffing context, material, construction details, and interruptions can also matter. This context turns a raw count into a planning indicator. It does not guarantee that the same output will be achieved on another shift, style, or production run.
Which Output and Time Measures Should You Track?
Choose the measure according to the decision being made. Capacity planning may require accepted operations per scheduled hour. A process investigation may instead compare output during machine-running time with output over the full observation window. Quality planning may require both total completed operations and accepted operations so that apparent gains are not created by counting rejected or reworked output as equivalent to good production.
| Measure | What to record | Planning use |
|---|---|---|
| Total output | All completed units, with the unit explicitly defined | Shows gross production activity |
| Good output | Units accepted under the stated quality rule | Shows usable sewing operation output |
| Elapsed time | Full start-to-finish observation period | Captures production as experienced during the observation |
| Scheduled time | Time assigned to production, with planned exclusions stated | Supports staffing and schedule comparisons |
| Machine-running time | Periods when the machine is operating | Helps separate sewing activity from interruptions |
| Labor time | Operator or team time assigned to the work | Supports labor-focused planning |
Direct observations and calculated indicators should remain separate in the record. Counts, timestamps, accepted quantities, and interruption notes are observed facts. A rate calculated from those facts is an indicator whose meaning depends on the selected denominator. If output is reported per machine-running hour, it should not be compared directly with a rate based on scheduled time.
Productivity, utilization, and efficiency are related concepts, but they are not interchangeable labels. A study should define exactly how each term is being used before presenting a comparison. Avoid assuming that another factory, software system, or production report uses the same definition.
For example, a hypothetical run producing 240 accepted operations over four elapsed hours would be reported as 60 accepted operations per elapsed hour. This example assumes each accepted operation is counted once and rework or rejected output is excluded. Changing either the output rule or the time basis changes the indicator.
How Can You Measure Productivity During a Representative Production Run?
Begin by stating the question. Are you estimating planning capacity, investigating lost time, comparing production conditions, or checking whether a recent change produced a different result? Then define the felling operation, output unit, quality rule, observation window, and comparison baseline before collecting data.
- Identify the production context. Record the style or product, material, seam or construction being processed, machine identification if relevant, and operator or staffing arrangement.
- Mark the observation boundaries. Note the start and finish times and whether the window represents elapsed, scheduled, running, or labor time.
- Count output consistently. Record total completed output and, when relevant, accepted, rejected, and reworked quantities separately.
- Log interruptions. Distinguish machine stoppage from waiting for work, changeover, adjustment, material shortage, inspection, or another observable event.
- Check the record. Reconcile the observation with available production or quality records and identify missing counts, estimates, or conflicting entries.
- Report conditions with the rate. Preserve enough context for another planner to understand what the result represents.
Observe normal production across the conditions relevant to the decision. A short, carefully prepared trial may show what happened during that trial, but it should not automatically be treated as representative of a shift or style. There is no universal observation duration suitable for every factory and question. Unusual events should be documented rather than silently removed; if they are excluded from a calculation, state the exclusion and reason.
What Production Conditions Change the Measured Result?
Felling machine production factors extend beyond the equipment itself. Operation difficulty, garment construction, material behavior, workpiece handling, seam length, and required quality can change the time needed for each unit. Operator familiarity, work method, staffing, material availability, and upstream or downstream flow can also affect measured output.
Classify lost time before interpreting it. A machine fault, waiting for components, style changeover, adjustment, thread replacement, quality check, and lack of downstream space are different production events. Combining them into one downtime total may hide the condition that planners actually need to investigate.
Quality observations also require caution. Seam puckering, for example, can have more than one potential contributor, including tension, feeding behavior, construction density, or differential shrinkage. A similar appearance on two garments does not establish the same cause, and one defect does not by itself prove a machine fault.
Needle, thread, fabric, stitch settings, handling, and operating conditions interact. They should be checked using the intended material, construction, and production conditions rather than judged in isolation. Record suspected variables, compare controlled samples where practical, and avoid attributing a productivity change to one setting or component without supporting observations.
How Should You Compare Shifts, Styles, or Machines Fairly?
A comparison is meaningful only when the compared results describe substantially similar work. Align the operation definition, output unit, time basis, quality rule, and production context before deciding that one shift, style, or machine performed better. A result reported as completed garment pieces should not be compared directly with a result reported as seams or operations, even when both came from the same production area.
Record the work content as carefully as the machine identity. Style, garment construction, material behavior, seam length, workpiece handling, operator experience, staffing, and material availability can all change the observed rate. Interruptions also need their own descriptions. Waiting for components, changeover, adjustment, thread replacement, quality checking, and a machine stop are not interchangeable losses.
A simple comparison log can include the date or shift, style and operation, material, staffing context, observation time, total output, accepted output, rework or rejected pieces, interruptions, and notes. These fields help separate a change in the work from a change in machine performance. They also make the result easier to review when production records and floor observations do not match perfectly.
Small or unusual observations should be treated as directional evidence. For example, a hypothetical short run on a simple lightweight style may appear faster than a longer run on a layered or difficult construction, but that difference does not establish that one machine is inherently more productive. Repeat the comparison under reasonably comparable conditions and state what could not be controlled.
How Do You Turn Productivity Data Into a Production Plan?
Use a representative observed rate as a planning input, not as a guaranteed target. Before using it, confirm that the output unit and time basis match the production requirement. A rate for accepted operations during machine-running time cannot be transferred directly to a demand calculation based on scheduled shift time unless the difference in time basis is understood and documented.
Capacity planning should keep its assumptions visible. Note the style or operation, expected staffing, available production time, quality criteria, and the interruptions included in the observation. Any buffer should be chosen for the particular project and uncertainty involved; there is no universal allowance that applies to every factory, product, or felling-machine setup.
When the measured result is below the planning need, investigate the largest documented losses first. Waiting, setup, handling, quality correction, material shortages, and flow imbalance may be more important than the machine’s nominal capability. Machine replacement or adjustment should not be treated as the automatic answer when the records point to an upstream shortage or a downstream constraint.
After a process change, measure production again under comparable conditions. Track accepted output alongside total output, rework, and defects so an apparent increase in speed is not separated from its quality consequences. Keep the source of each figure clear: an observed count, a production record, a calculated indicator, and an editorial recommendation are different kinds of information.
Apparel Wiki is an independent garment-industry knowledge blog, not a manufacturer, factory, equipment supplier, laboratory, or certifier. Its guidance can help readers structure a planning question, but equipment-specific decisions require information from the responsible production and technical teams.
What Can Productivity Measurements Not Tell You?
A short observation cannot represent every style, operator, shift, material, or production stage. Even a carefully recorded result describes the conditions that were observed. It does not automatically predict another order, a different material lot, or a later production period.
High gross output alone does not establish good quality, low cost, balanced flow, or sustainable performance. If rework and rejected pieces are included in the count, the reported result may look stronger than the accepted output available for the next operation. The measurement should state how those pieces were treated and which quality rule was applied.
A machine-level result also cannot explain the whole line by itself. Upstream shortages, downstream bottlenecks, labor allocation, inspection queues, and material movement can limit output without indicating a mechanical problem. Conversely, a machine stop may be only one part of a broader production issue.
State missing data, exclusions, estimates, and assumptions with the result. When the evidence is incomplete, the next useful step may be another comparable observation, a focused review of one documented loss, or qualified technical support for an equipment-specific concern. Clear limits make a productivity measure more useful because they prevent readers from treating it as a complete performance judgment.
For a practical follow-up, organize the observation fields in a repeatable worksheet and review related Apparel Manufacturing Tools where appropriate. Keep the original counts, conditions, and quality notes together so future comparisons can be made on the same basis.
Frequently Asked Questions
What is a felling machine in garment production?
A felling machine is a sewing machine used for specific garment construction operations that join, fold, or finish fabric edges or seams, depending on its configuration and application. The exact work content should be defined before measuring its productivity.
How do you calculate felling-machine productivity per hour?
Count a clearly defined output, such as accepted operations or completed components, and divide it by the stated time basis. Identify whether the time is elapsed observation time, scheduled time, or machine-running time so the result is interpretable.
Should productivity be based on total output or accepted output?
Record both when quality losses matter. Total output shows completed work, while accepted output shows what passed the stated quality rule. Reporting only one can hide rework, rejection, or correction requirements.
How long should a production observation last?
There is no single duration suitable for every factory or planning question. Observe enough normal production to capture relevant cycles and interruptions, and report the actual observation period, unusual events, and any gaps or estimates.
Why can the same machine produce different output on different styles?
Style construction, seam length, layers, material behavior, handling, quality requirements, operator familiarity, staffing, and production flow can all change the time per operation. A different output rate does not by itself prove a machine difference.
Does higher machine output always mean better production performance?
No. Higher gross output may occur with more rework, defects, waiting elsewhere in the line, or unsustainable operating conditions. Compare accepted output, quality, interruptions, and flow context before judging overall performance.